In a factory, a flour mill, a brewery, a pumping station, a cement works, a quarry or a packaging line, machines wear, heat up, vibrate and eventually stop. The industrial maintenance provider — electromechanical technician, mechanic, hydraulics specialist, as the case may be — is the one the operator calls so that it does not happen, or so that it lasts as short a time as possible. Two logics compete in this trade: intervening when it breaks, or intervening before. It is that opposition that decides the provider’s value and what the customer agrees to pay for — and it is where one has to start.
Corrective: repairing when it breaks
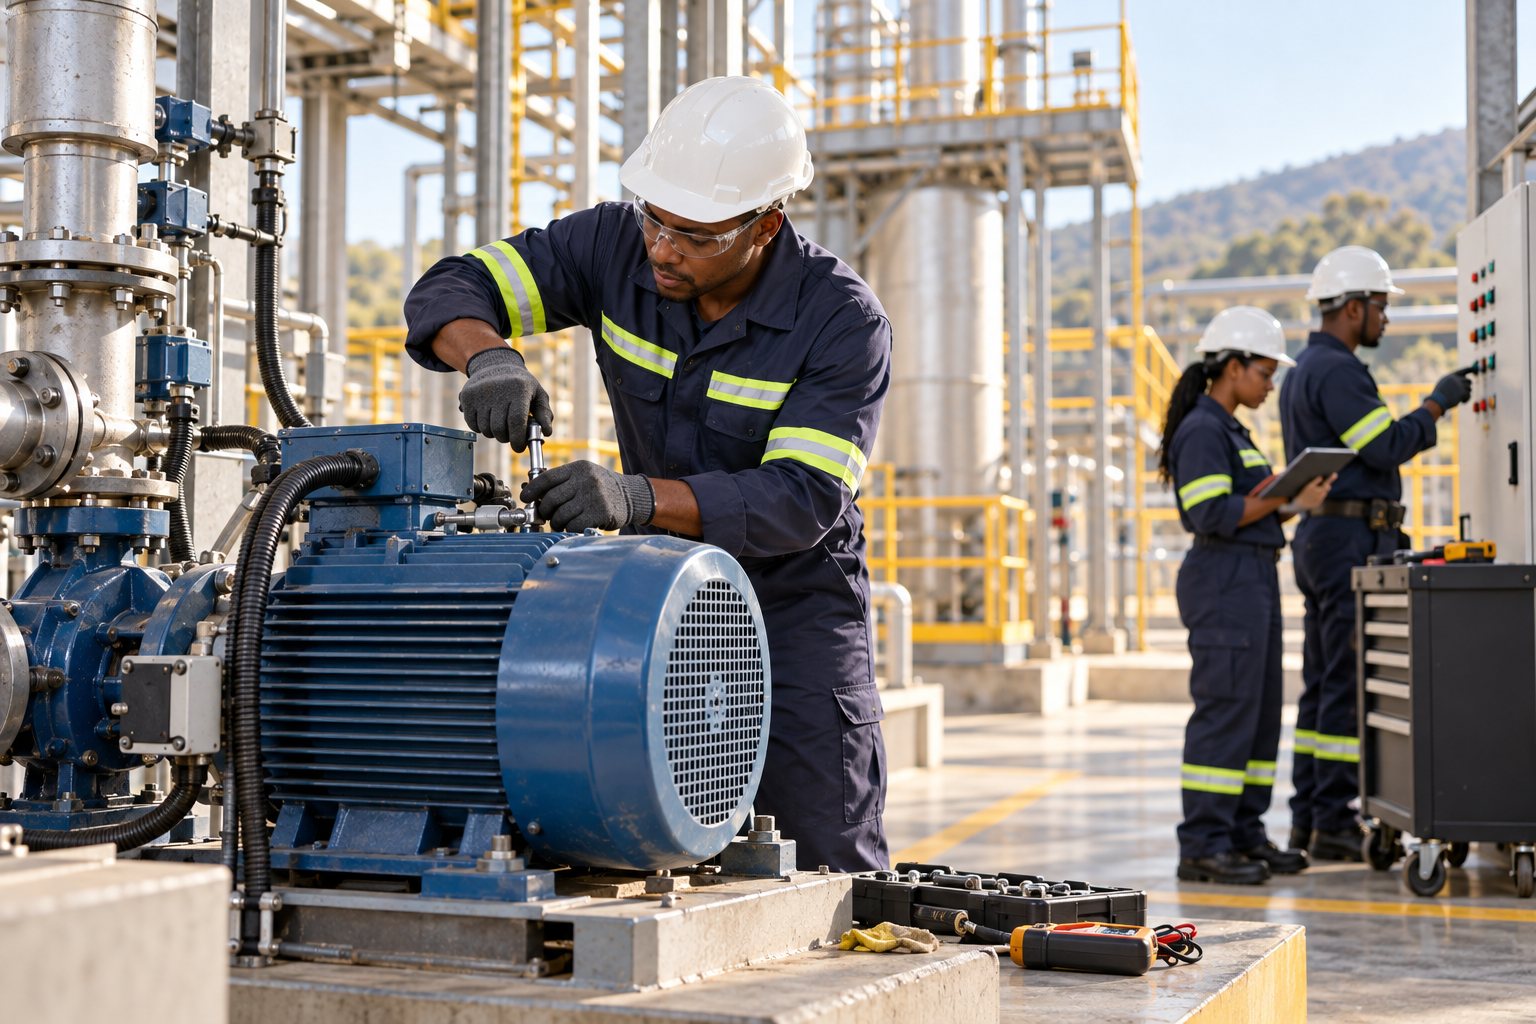
The call comes when the machine has stopped. The technician travels, listens to the operator, observes, measures, looks for the cause — mechanical, electrical, hydraulic, pneumatic, control — and repairs with what they have, or with what they have brought in. Corrective work is the most visible activity of the trade, the most urgent and the least profitable for everyone: the operator loses production, the provider works under pressure, and the part is rarely there at the right moment.
A good call-out nonetheless has its rules: do not restart without having understood, replace what caused the breakdown and not only what it damaged, and write down what happened. A call-out without an identified cause prepares the next one.
Preventive: intervening before
The other logic consists of establishing, for each machine, a plan: periodic inspections, lubrication, retightening, replacement of wear parts — bearings, belts, seals, filters, contactors — before they give way, measurements that reveal a drift — temperature, vibration, current drawn, pressure — and scheduled shutdowns for heavy operations. That plan is built from manufacturers’ recommendations, the breakdown history and actual operating conditions, and it is revised.
Preventive work costs money when nothing breaks, and that is precisely where the provider must convince: they sell an avoided stoppage, which is never seen. Their best proof is the history — how many unscheduled stoppages before the plan, how many after — and that is why they keep each machine’s records up to date.
Between fixed-date preventive work and corrective work lies a third way, condition-based maintenance: one intervenes neither on a date nor at the breakdown, but when a measurement says so — rising vibration on a bearing, climbing temperature on a journal, increasing current on a motor, a thermal image revealing a connection that heats up. It requires instruments and regular readings, but it avoids replacing parts that are still sound and letting parts age that no longer are. A provider who can read those measurements replaces parts at the right moment, neither too early nor too late.
Locking out before touching
No intervention begins on an energised machine. Lockout — cutting off, locking, tagging, verifying the absence of voltage, pressure, movement — protects the technician and the operators, and it protects the operator of the plant from an accident for which they would be liable. The ILO recalls that a safe and healthy working environment is a fundamental principle and right at work; in industry, that begins with lockout and continues with protective equipment, secured work at height, load handling and coordination with the plant operator: who stops the line, who authorises the restart, who warns the operators.
The provider who agrees to intervene “quickly, without stopping the machine” because production is pressing puts a life at stake. That is the first refusal the trade imposes, and it is prepared: a ten-minute stoppage planned with the production manager costs less than an accident, and the provider who obtains it explained why before arriving.
Parts: the stock decides the delay
A stopped machine often waits longer for a part than for a repair. The maintenance provider knows which wear parts its customers consume, keeps a stock or makes sure the operator keeps one, identifies exact references and suppliers, and distinguishes the original part, the compatible part and the reconditioned part — with what each is worth. The delay announced depends on that availability, and the provider says so rather than promising a restart that logistics does not allow.
Counterfeiting is a risk specific to industrial parts: bearings, contactors, belts and filters bearing a known brand circulate without having its quality, and fail within weeks. The provider buys from identified distributors, checks the markings, refuses parts whose origin cannot be established and says so to the customer tempted by a low price — because the provider is the one who will come back to repair.
Diagnosing with method
A pump that vibrates, a motor that overheats, a conveyor that stops for no reason: diagnosis goes from effect to cause, and the cause is rarely the first part affected. A bearing that fails may come from misalignment, an over-tensioned belt, missing lubrication; a motor that burns out, from overload, unbalanced voltage, a blocked ventilation path. The technician measures — alignment, voltage, current, temperature, vibration — rather than assumes, and documents: a breakdown diagnosed on a machine becomes a checkpoint in the preventive plan.
Skills, training, team
Industrial maintenance draws on several trades — mechanics, electricity, automation, hydraulics, welding — and a growing share of digital skills: drives, PLCs, sensors, supervision. The ILO stresses, in its work on skills and lifelong learning, that automation and technical change require workers who keep training; for a maintenance provider, that means training its technicians on its customers’ machines, keeping documentation up to date, and knowing when to call a specialist — automation engineer, refrigeration technician, manufacturer — when a fault exceeds the team.
The contract: scope, frequency, commitment
The maintenance contract describes the machines covered, the preventive plan and its frequency, the response time on breakdown, the consumables and parts included or not, the reports delivered, and what remains outside scope: heavy refurbishment, modification of a machine, breakdowns due to misuse. The price is built on the number and type of machines, the frequency, the distance and the level of commitment; there is no “industrial maintenance” tariff valid everywhere, and the provider does not claim one.
What the contract promises: a plan executed, interventions within a written time, traceability. What it does not promise: the absence of any breakdown. A machine can fail without warning; the contract promises that this will be rare, understood and quickly repaired.
The operator has their share
Maintenance is not only the provider’s business. The operator who runs a machine beyond its capacity, skips scheduled shutdowns, lets operators bypass a safety or does not buy the recommended parts undoes the plan. The ILO’s WISE programme shows that simple organisation of the workstation — cleanliness, tidiness, instructions, first-level upkeep by operators — improves both safety and productivity. The provider that trains operators for that first level — monitoring, greasing, cleaning, reporting — reduces its own call-outs, and that is the sign that it works for the machine and not for the invoice.
In the African context
On the continent, the first given of the trade is the age and diversity of the machines: equipment imported second-hand, lines of different makes assembled over successive purchases, documentation missing or in a language no one reads, original parts several weeks away by sea. The maintenance provider is often the only one who really knows a machine, and its value lies in the documentation it builds itself — surveyed diagrams, identified references, recorded settings — where the manufacturer left nothing.
Energy comes next: outages, surges, unbalanced voltages and poorly regulated generators are, in many plants, the first cause of wear on motors, drives and control boards. Part of the maintenance work consists of protecting the machines from the grid — regulation, protection, restart sequences — rather than repairing what it destroyed.
Skills, for their part, are built on the ground more than at school: technicians trained on the machines actually in service are rare, technical courses do not always keep up with the equipment, and the provider that trains its own technicians, machine by machine, customer by customer, creates know-how the market does not supply. The ILO recalls that lifelong learning is a necessity for workers facing technical change; in an African plant, it is a necessity for the plant itself.
What remains when the technician has left
Two plants, the same pump, the same bearing failure. In the first, the technician replaced the bearing, restarted and signed a one-line job sheet; six months later the bearing fails again, nobody remembers the cause, and the same bearing is bought again. In the second, the report says the bearing failed from misalignment, that the alignment was redone, that the belt was over-tensioned and that a vibration check is planned in three months; the next bearing lasts for years.
The difference between the two plants lies neither in the technician nor in the bearing. It lies in what remains on the table when the technician has left — and that, in the end, is what the operator buys.